In cardboard, paper and tissue production, large exhaust air streams are generated that are laden with dust, fibres and other particles. This exhaust air must be treated reliably without placing an unnecessary burden on the ongoing production process. The automatic drum filter solution from bg filtration combines high air performance with continuous filter cleaning, controlled dust removal and a compact design. As a result, it can also be used where high demands and limited space coincide.
High air volumes, varying particle sizes and continuous production operations make exhaust air filtration demanding. A single standard component can often not fully cover these requirements. If the solution is not appropriately designed for the application, maintenance effort increases, separated dust can accumulate in the system and integration into existing ductwork becomes unnecessarily complex. Therefore, what is decisive is not only the performance of the filter, but the coordinated interaction of pre-separation, filtration, cleaning, dust discharge and air routing.
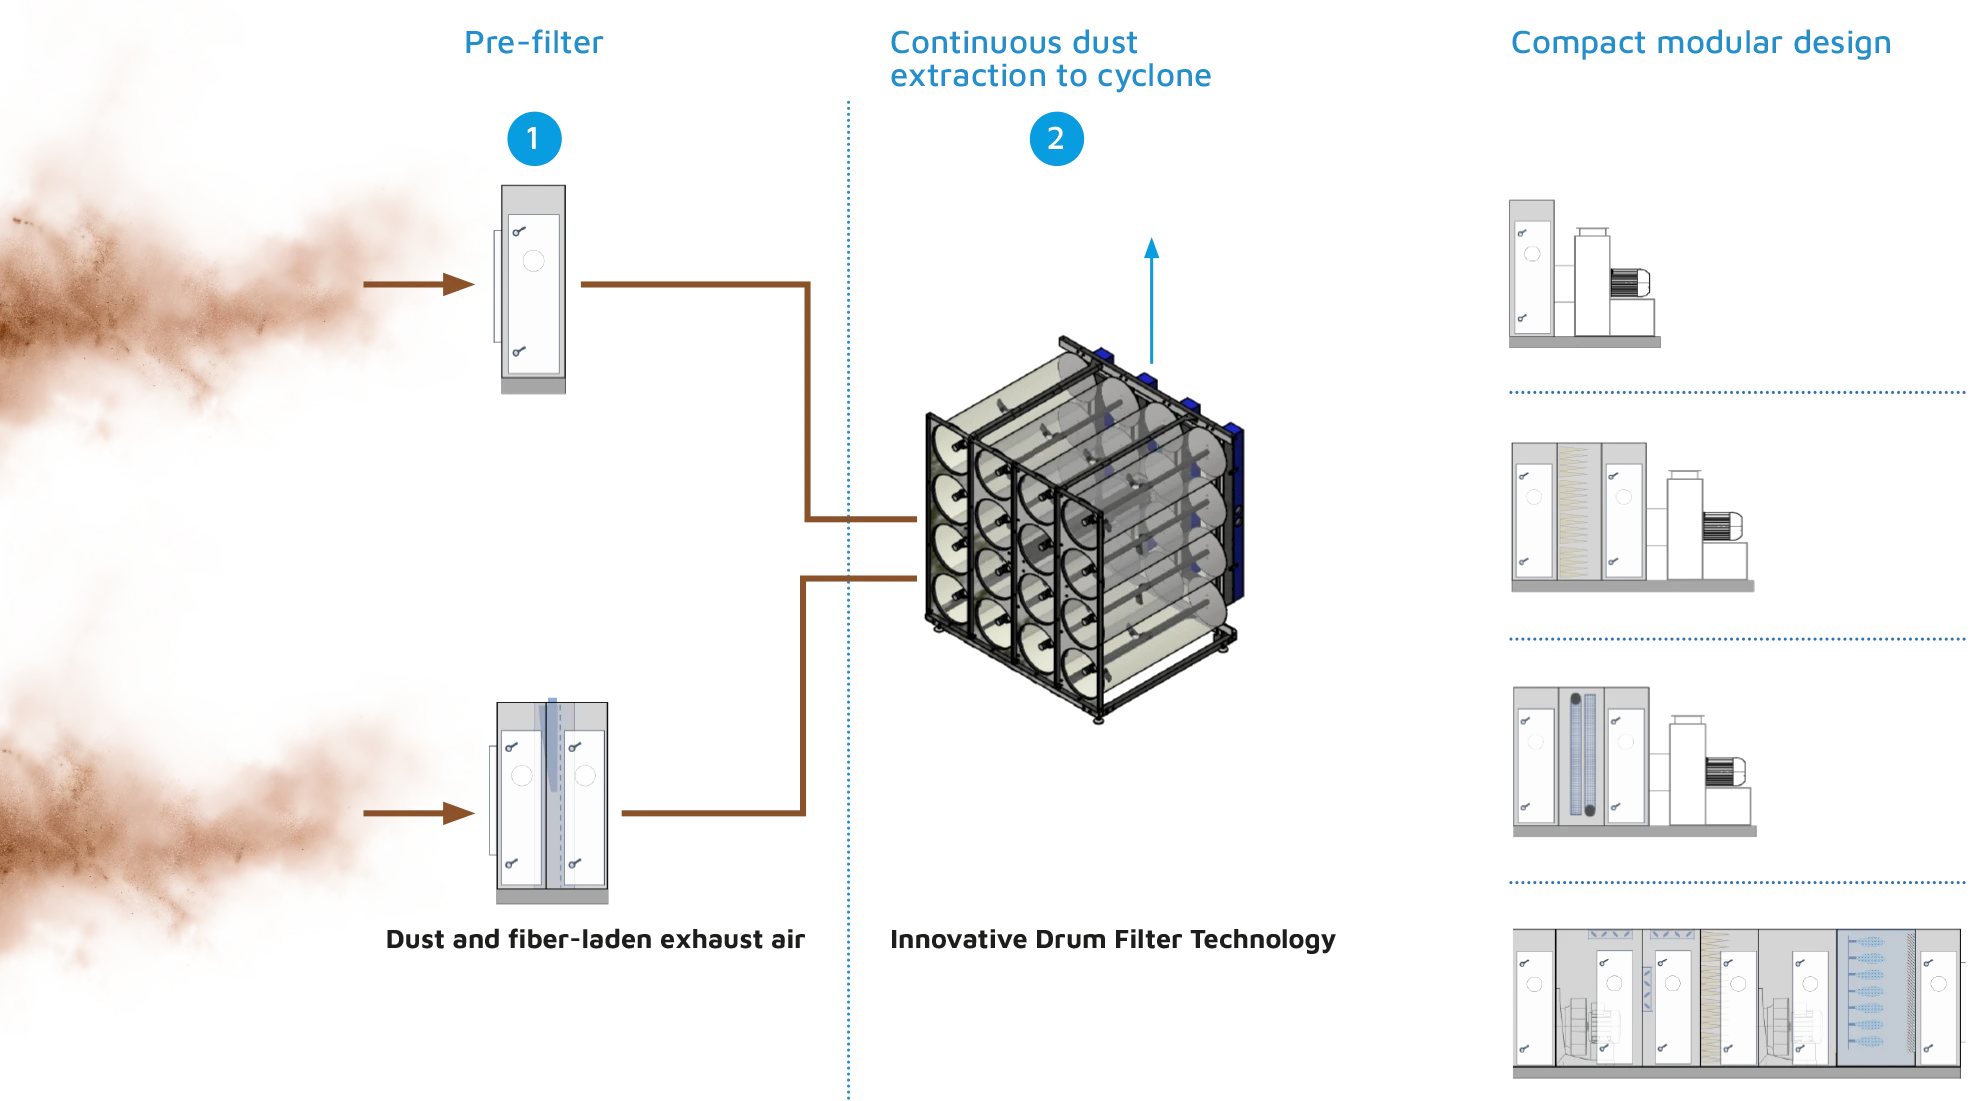
With the automatic drum filter technology VersaDrum VDF-8 / VDF-16, bg filtration uses proven components to develop a solution that can be tailored to the specific application. The contaminated air is routed from the inside outwards through the drum filter and is reliably cleaned in the process. The filter medium is cleaned automatically, while the separated dust is continuously discharged from the system. Depending on the process, pre-filters, cyclones, post-filtration, heat recovery and other air treatment modules can be integrated. This creates a cohesive system that does not end with filtration, but also takes into account the further use or discharge of the purified air.
The solution is of interest to companies that need to handle high air volumes reliably while keeping capital, space and operating costs in mind. Depending on the configuration, up to 60,000 m³/h can be processed per filter unit. The compact, modular design facilitates integration into existing production environments and enables a needs-based layout without planning unnecessary functions or oversized system components. Automatic filter cleaning and continuous dust removal support stable operation with fewer manual interventions. Additions such as heat recovery or the recirculation of cleaned air can create additional efficiency potentials. At the same time, the system remains adaptable if production conditions or requirements change later on.
Technically crucial is the controlled routing of the laden air through the entire system. In the drum filter, it flows from the inside outwards through the filter medium. Rotating nozzles automatically clean the medium under negative pressure so that the filtration process is continuously supported. The separated dust is continuously conveyed to the cyclone, separated there and then discharged in a controlled manner via a rotary valve or a dust compactor. For larger fibres or particles, a pre-filter can be installed upstream. Depending on the clean air requirement, additional filter stages up to HEPA, a finned-tube heat exchanger made of 316 stainless steel as well as modules for air conditioning, air scrubbing or humidification can be integrated. The specific design takes into account air volume, dust and fibre load, temperature, air flow and existing interfaces. An ATEX-compliant version is possible and is checked on a project-specific basis.
The drum filter solution is particularly suitable for dust- and fibre-laden exhaust air in the cardboard, paper and tissue industries. It is designed for applications where high air volumes need to be treated reliably and continuously.
Depending on the configuration, up to 60,000 m³/h per filter unit is possible. The actual design depends on the air volume, temperature, dust load and the requirements for the cleaned air.
The separated dust is continuously extracted to the cyclone, separated there from the air flow and subsequently discharged in a controlled manner. This prevents an accumulation of material in the filter area.
The modular system architecture enables adaptation to existing air ductwork, spatial conditions and other system components. Depending on the design, the cleaned air can be discharged to the outside or recirculated back into production.
Depending on the application, pre-filters, additional filter stages up to HEPA, heat recovery and further modules for air conditioning can be added. The solution can thus be adapted to different process and clean air requirements.
An ATEX-compliant version is available. The specific design is determined based on the application, the dust properties and the project-specific safety requirements.
Is your extraction system too complex for a standard solution?
When high air volumes, dust, fibres, limited floor space and requirements for safety or clean air come together, a solution is needed that considers all these factors collectively. Talk to bg filtration about your application. Based on air volume, dust load, temperature, airflow and installation situation, we will determine which combination of drum filter and supplementary system components makes sense for your process.
Enquire about a bespoke system solution now
The right filter system is a decisive factor for the safety of machines, processes, product safety and the health of your employees. Errors in the filter configuration can have a decisive impact on these factors. Only specialists work for us; our modular systems have been tried and tested in industry and are of the highest quality.
Pascal Wieland
Pascal Wieland
Key Account Manager and Product management
Tel +49 7159 8069-25
Mobile +49 162 3017787
pascal.wieland@bg-filtration.de